Your Reliable EVA Case Manufacturing Partner
The dedicated custom protective case and export manufacturing division of Dongguan Flame Bright Sports Products Co., Ltd., supporting global B2B brands with full-cycle tooling, thermoforming, and precision fabrication.
Located at Room 301, Building 1, No. 102 Chashan Jinshan Road, Chashan Town, Dongguan City, our facility combines two decades of industrial foam molding expertise with strict ISO-based quality control. Led by founder Harry—a former SOE plant director and certified ISO 9000 Lead Auditor—we deliver engineered EVA storage cases, custom foam inserts, and protective packaging solutions built for demanding commercial specifications.
Who We Are
We are a manufacturing-focused team specializing in custom EVA cases for electronics, medical devices, tools, eyewear, audio products, and other B2B applications. We help buyers turn product protection needs into practical case solutions.
Why Buyers Choose Us
We combine practical engineering, efficient communication, and repeatable manufacturing processes to support both new product launches and long-term buyers.
OEM / ODM capability
Fast Sampling
Stable Production
Quality Control
Export Experience
Responsive Communication
Factory Snapshot
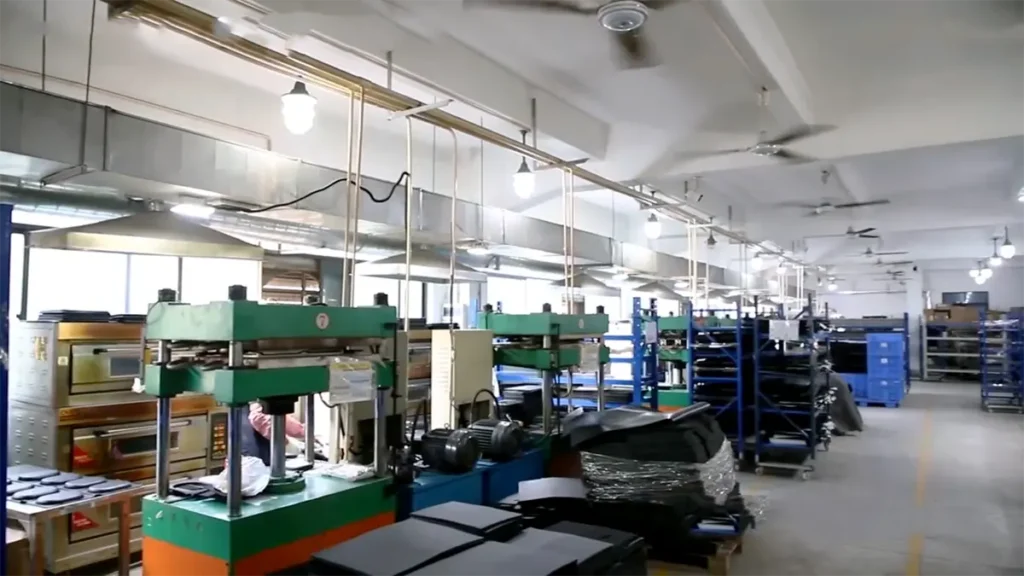
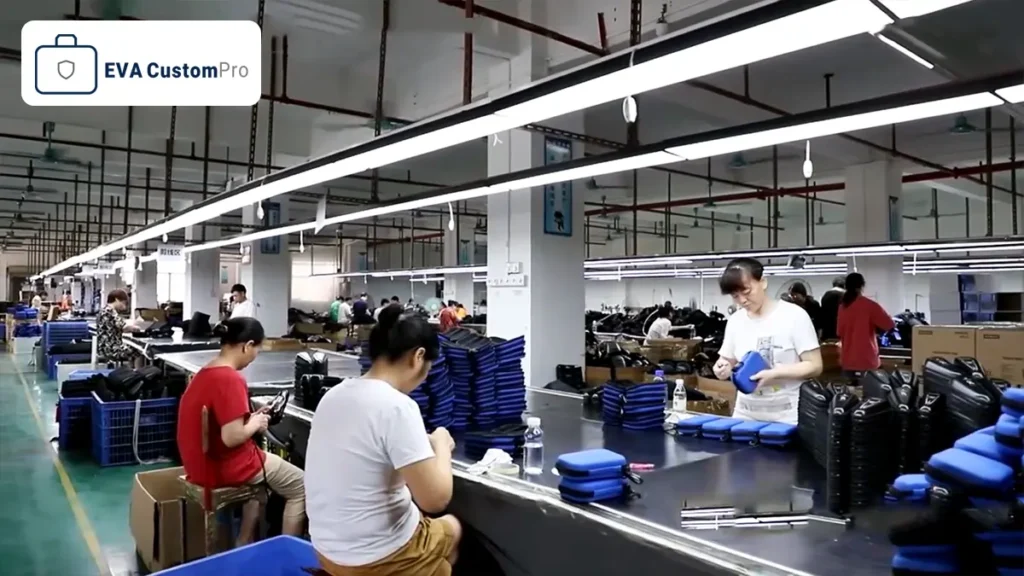
Our facility is designed to support structured production, quality checks, and consistent project execution from sampling to shipment.
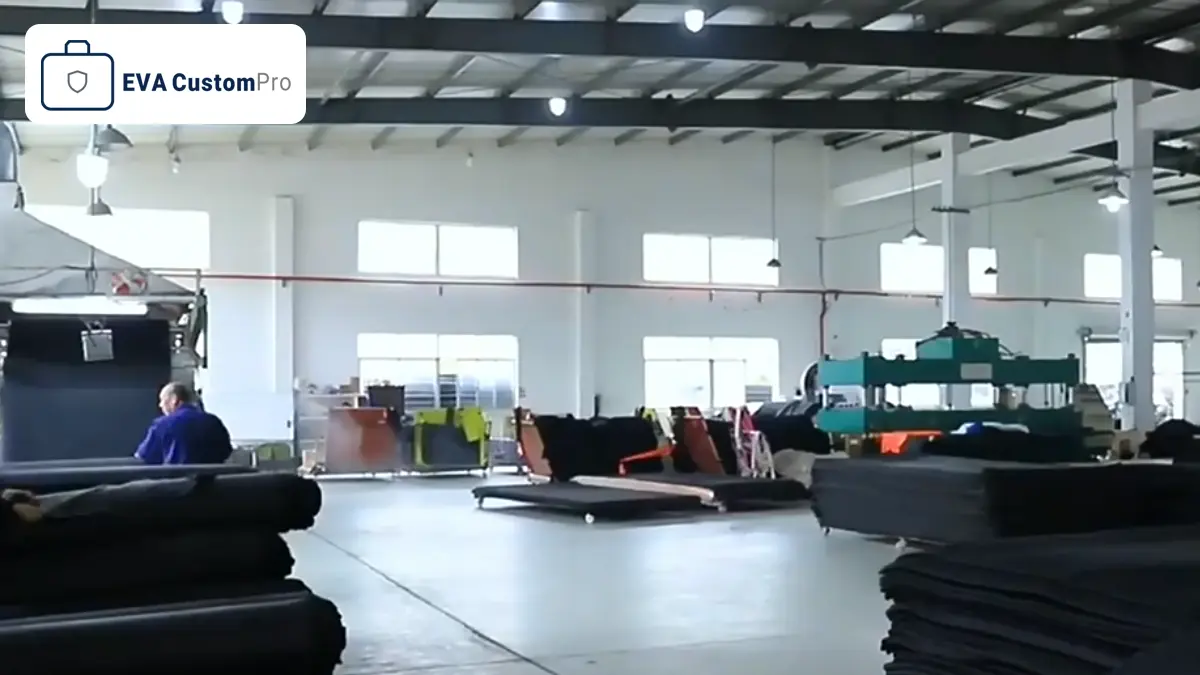
Workshop area
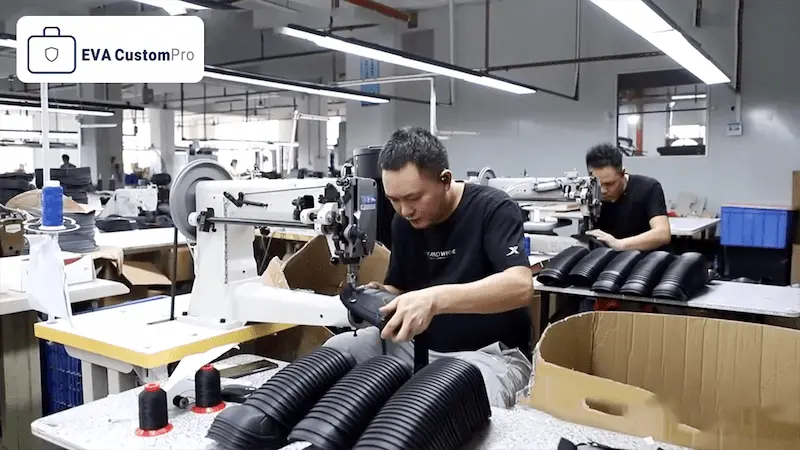
Production lines
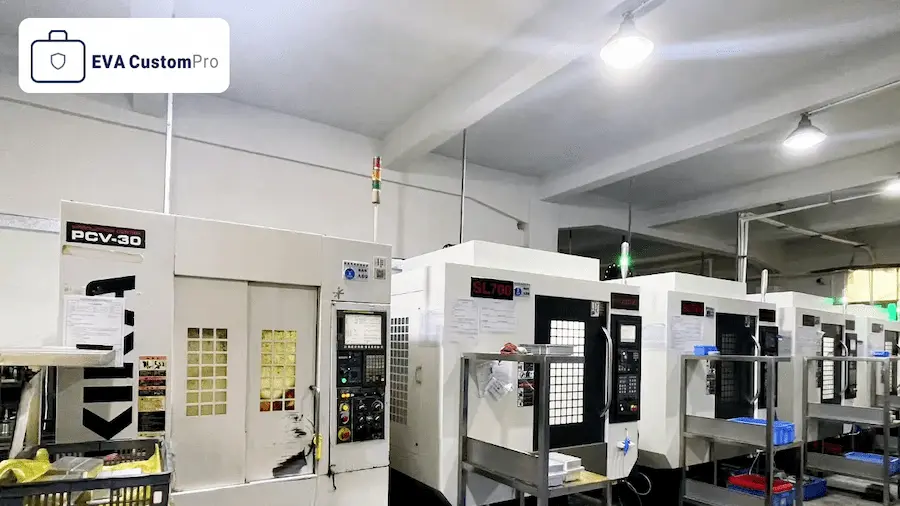
Equipment photos
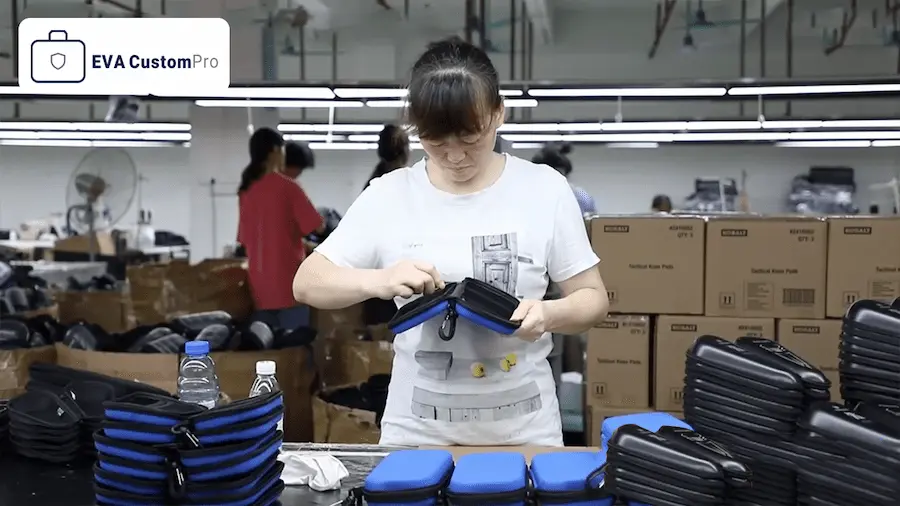
QC area
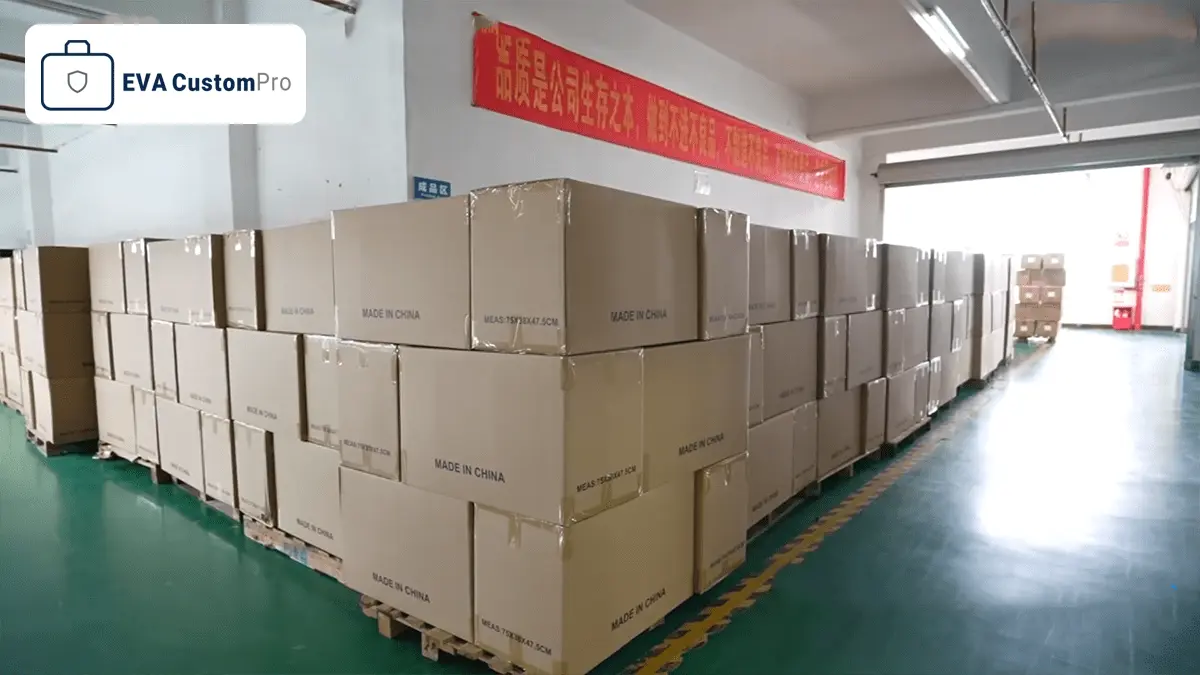
Warehousing
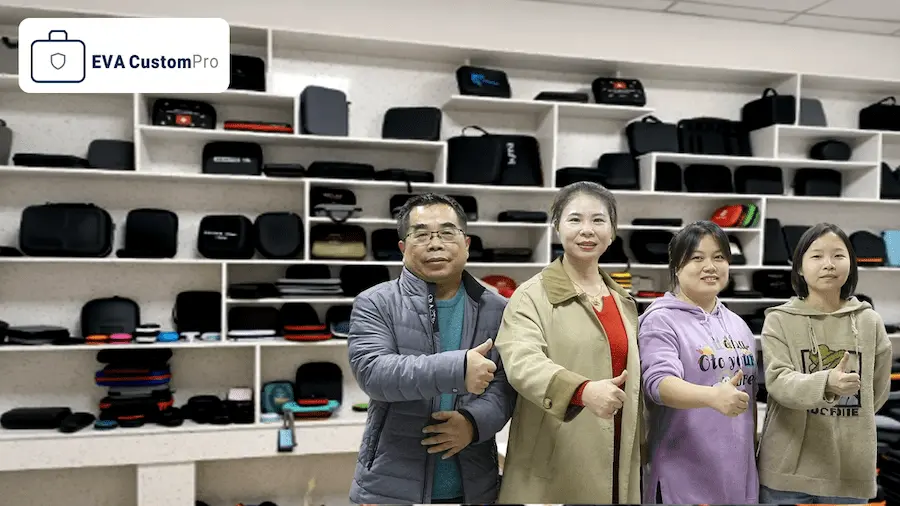
Team photos
Built for Scalable Production
Our production system is designed to support prototype development, pilot runs, and repeat production with consistent quality and lead time.
- Small-batch support.
- Mass production.
- Repeat order stability.
- Custom project handling.
- Lead time management.
Quality Control
We maintain a complete quality management system and strictly implement quality control procedures throughout the process, from raw material inspection to final inspection, to ensure consistent and reliable product quality.
End-to-End Quality Assurance
Strict inspection protocols applied at every stage of manufacturing to ensure zero-defect custom EVA cases.
Incoming Material Check
Inspect raw EVA sheets, fabrics, zippers, and hardware before production begins.
In-Process Inspection
Monitor thermoforming, die-cutting, logo printing, and stitching accuracy in real time.
Final Inspection
100% full check on finished case structure, foam insert fit, zipper smoothness, and aesthetics.
Packaging Check
Verify polybag sealing, carton strength, labeling accuracy, and protective packing.
Sampling Verification
Random AQL sampling before shipment to guarantee batch consistency and client standards.
Certifications & Compliance
We maintain relevant quality and material documentation to support international B2B procurement requirements.
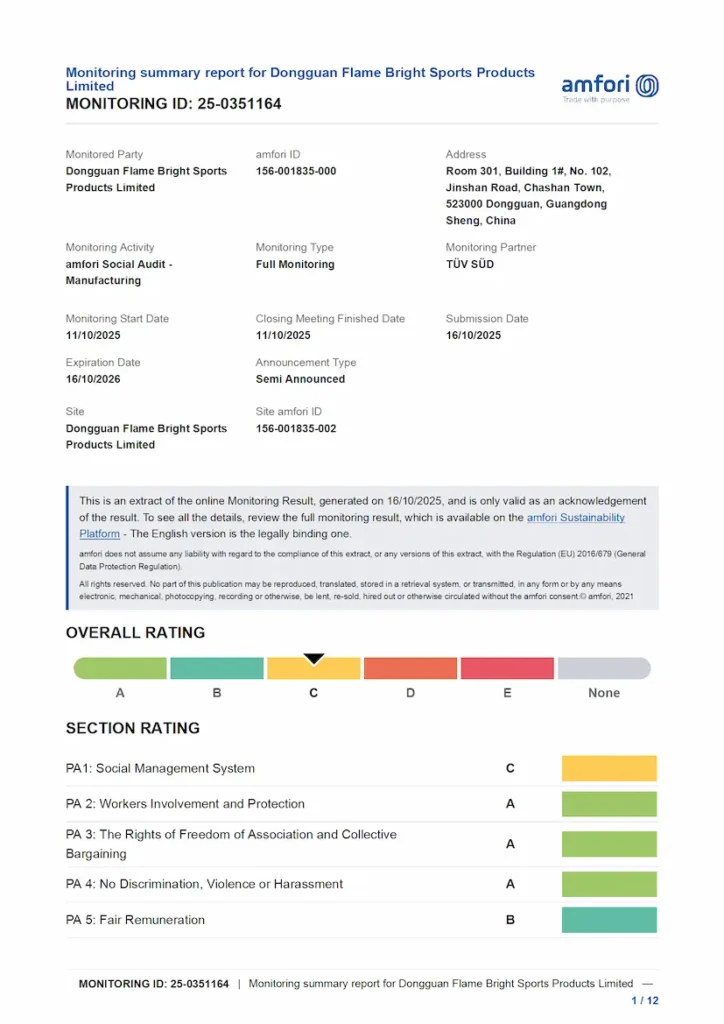
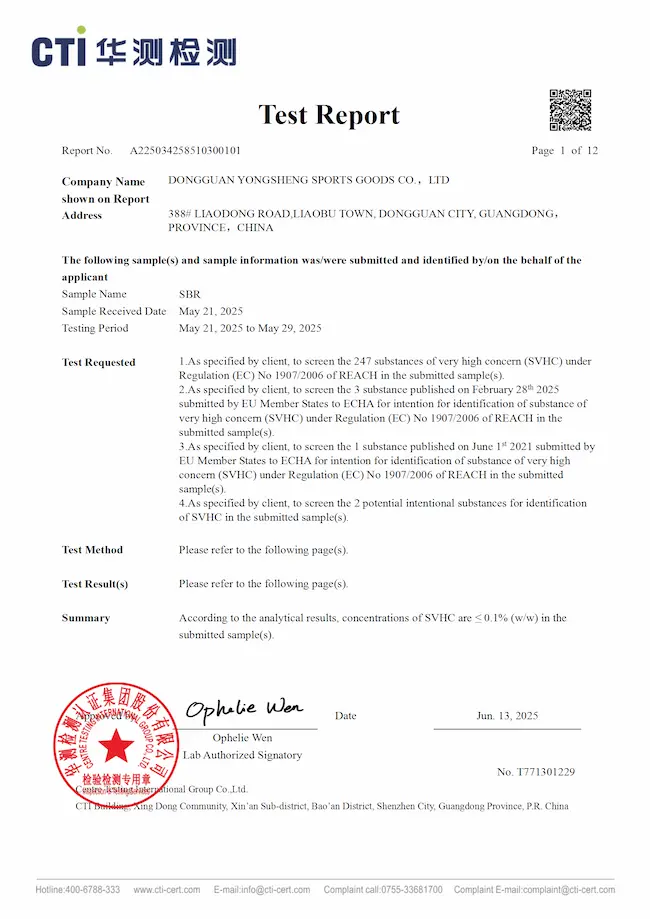
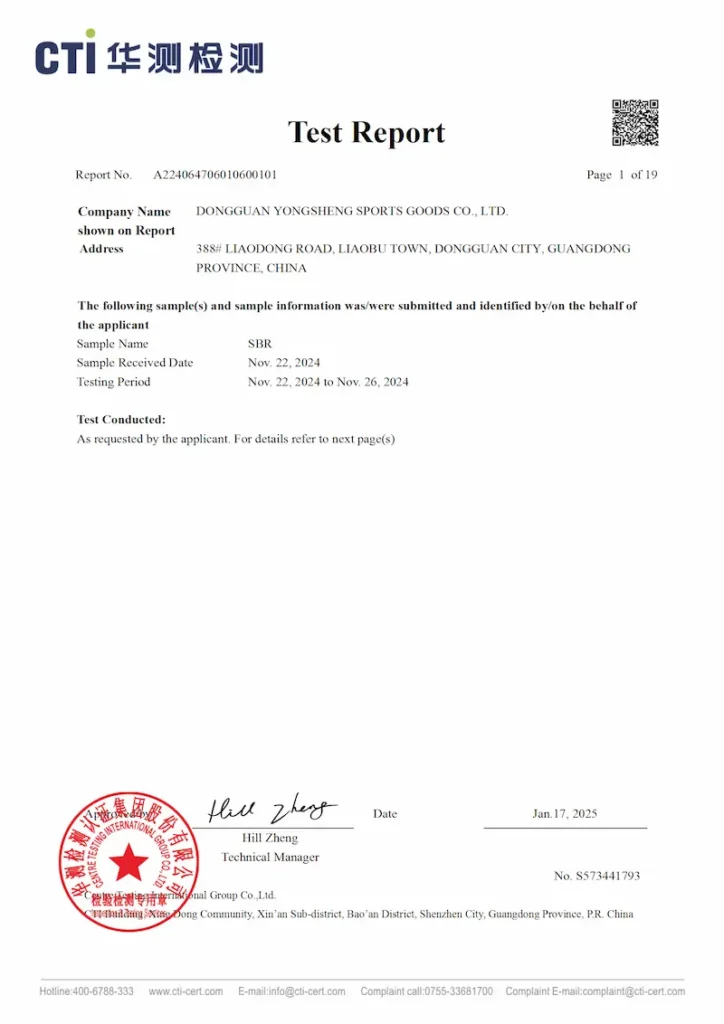
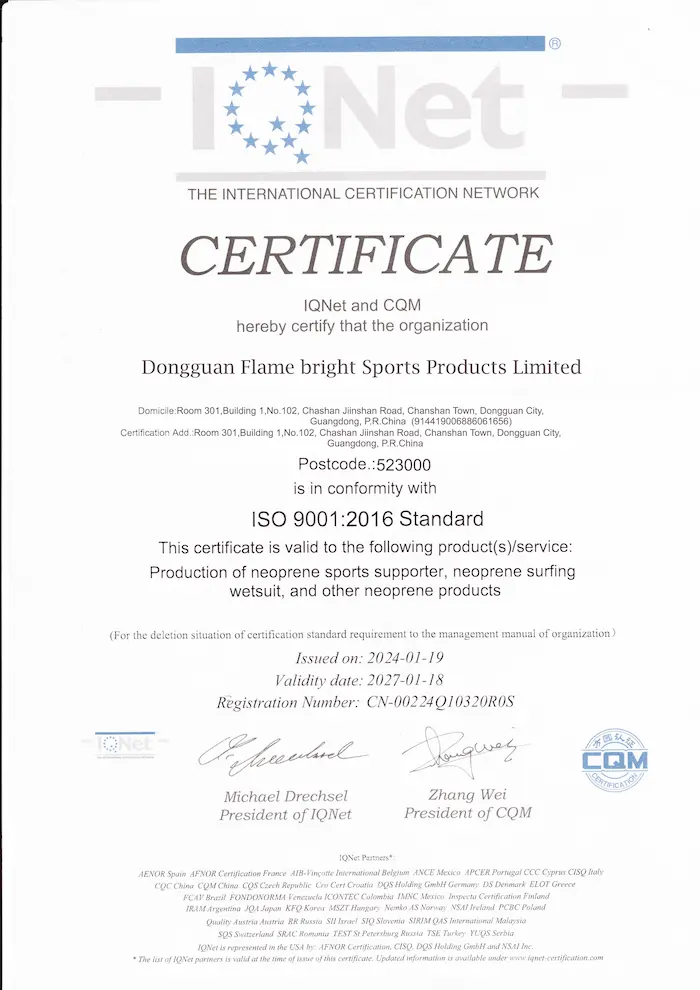
ISO 9001:2016 QMS Certificate
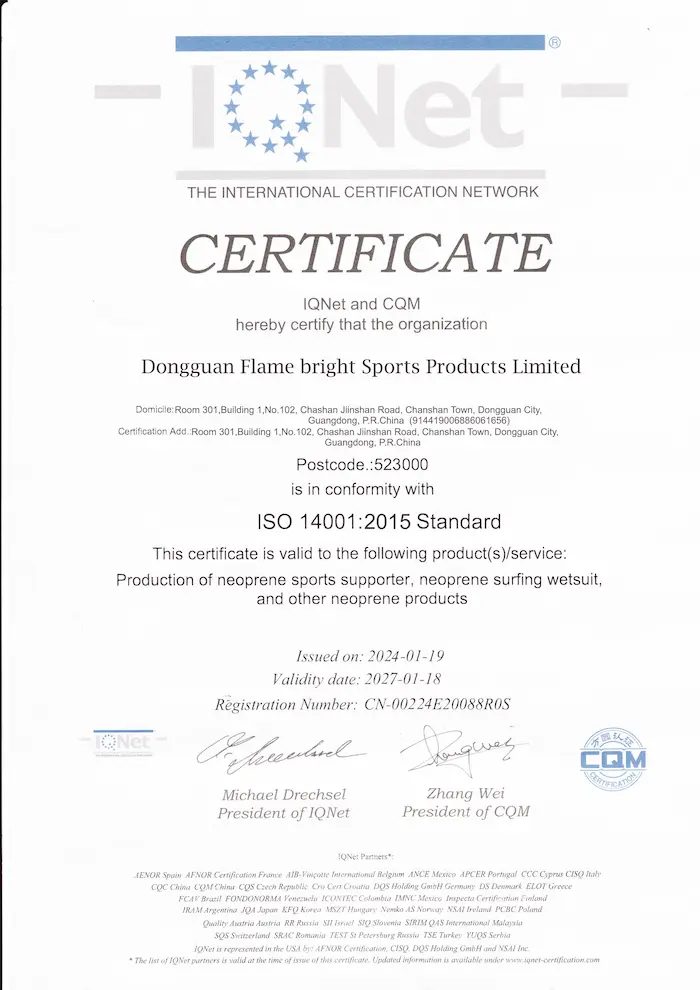
EMS Certificate (IQNet / CQM)
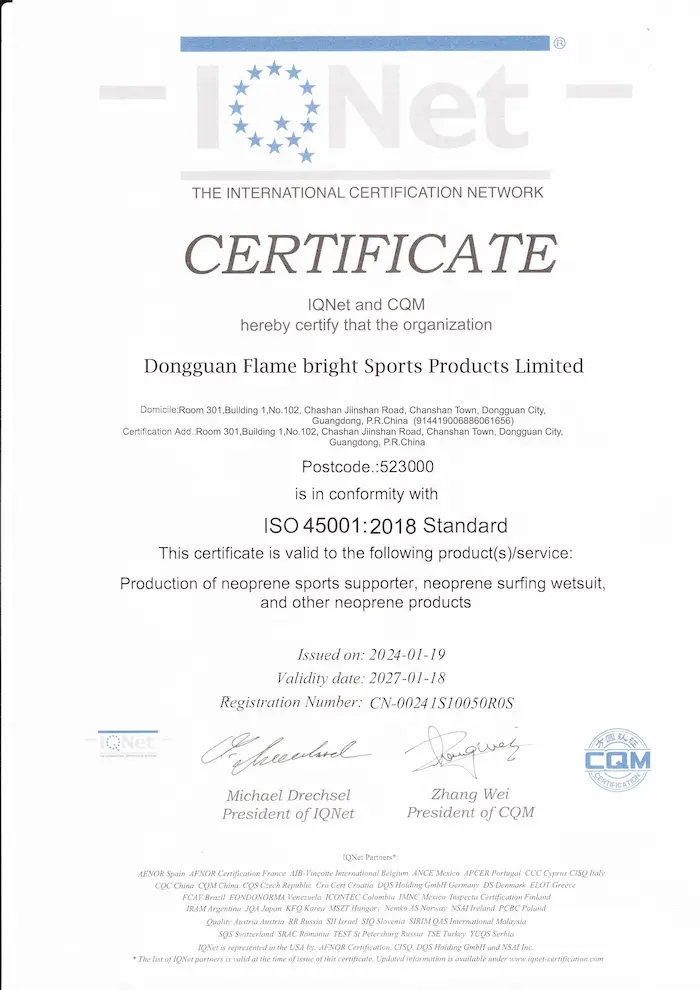
OHSMS Certificate (IQNet / CQM)
A Team That Understands B2B Projects
Our team supports project communication, sample coordination, production follow-up, and export-oriented service to help buyers move faster from inquiry to delivery.
- Sales / project team:Coordinates inquiries, samples, and communication.
- Engineering support:Reviews technical details and custom requirements.
- QC team:Monitors quality during production and final inspection.
- Production team:Ensures stable manufacturing and on-time delivery.
How We Work
A clear workflow helps reduce uncertainty and keeps projects moving smoothly.
Inquiry and requirement review.
Send us your product dimensions, application, and customization needs.
Design confirmation.
We confirm the structure, materials, insert layout, and key details.
Sample development.
We create prototypes for testing and approval.
Mass Production
After confirmation, we move into mass production.
Quality Check & Shipment
We inspect the products and arrange delivery according to your schedule.
Relevant Project Experience
We have worked on custom EVA case projects for different industries, each requiring specific structure, protection level, and presentation needs.
Frequently Asked Questions
We manufacture custom EVA cases for B2B applications.
Yes, we support both OEM and ODM projects.
Yes, we develop samples for review and approval.
- Usually, it takes 25–30 days. The exact timeline may vary depending on the product type, structure, and customization requirements.
We have a complete quality management system in place. From raw materials to production, we strictly follow quality control procedures at every stage. Before shipment, we carry out a final inspection to ensure the finished products meet our standards.
Yes, we support international export orders.
Yes, factory tours can be arranged.
We handle custom EVA case projects across multiple industries.
Have a project in mind? Contact us for a quick quote and support.
Send us your project details, and our team will help you with design, sampling, and production support.
EVA CustomPro™ Engineering Audit Summary | Digital Fast-Track
Page Topic
- Product: Custom EVA Cases — protective carrying and storage solutions built from high-density EVA (Ethylene-Vinyl Acetate), available in hard shell, carrying, storage, and organizer configurations, engineered for product protection, portable transport, and professional brand presentation across multiple B2B applications.
- Audience: Electronics brands, medical device manufacturers, tool distributors, eyewear companies, audio equipment suppliers, and B2B buyers seeking OEM/ODM custom EVA case programs with reliable quality, flexible customization, and scalable manufacturing support.
- Page Purpose: To build trust and credibility by presenting the factory as a reliable, manufacturing-focused EVA case partner — transparently communicating production capability, quality infrastructure, team expertise, and project experience to convert inbound traffic into qualified B2B inquiries.
Core Manufacturing Capabilities
- OEM / ODM Manufacturing: Full-spectrum support for both OEM (client-provided specifications) and ODM (design and engineering from concept to production) project models — enabling flexible collaboration for new product launches and existing product line upgrades.
- Custom EVA Case Production: End-to-end manufacturing of protective EVA cases across four structural categories — Hard EVA Case (rigid impact resistance), EVA Carrying Case (portable everyday use), EVA Storage Case (space-efficient organization), and EVA Organizer Case (compartment-based accessory management).
- Fast Sampling: Accelerated sample development cycle for design confirmation and fit validation prior to mass production — reducing project lead times and improving accuracy.
- Stable Production: Structured production systems designed to support prototype development, pilot runs, small-batch orders, and large-volume repeat production with consistent quality and predictable lead times.
- Quality Control at Every Stage: Multi-stage inspection protocol — incoming material verification, in-process production checks, final inspection, packaging verification, and pre-shipment random sampling.
Factory Infrastructure & Production Capacity
- Facility Overview: Manufacturing facility designed to support structured production workflows, quality inspection stations, warehousing, and export-oriented logistics coordination.
- Production Lines: In-house production capabilities including EVA sheet cutting, molding, lamination, stitching, assembly, and finishing — all integrated under one roof for better quality control and shorter lead times.
- Equipment & Tooling: Dedicated tooling for custom case dimensions, insert configurations, and hardware integration — with tooling retention for efficient reorder processing.
- Production Capacity: Scalable capacity for both small-batch pilot projects (flexible MOQ) and high-volume repeat orders — with export-oriented production scheduling.
- Export Logistics: Complete export documentation (commercial invoice, packing list, bill of lading); flexible shipping terms (FOB, CIF, EXW); container load planning; global shipping coordination across North America, Europe, Asia-Pacific, and other international markets.
Quality Control System
- End-to-End Quality Assurance: Quality leadership led by a national-level quality management auditor and training instructor — ensuring systematic quality oversight across the entire production lifecycle.
- Incoming Material Check: Verification of EVA sheet density, fabric quality, hardware specifications, and raw material compliance prior to production release.
- In-Process Inspection: Production-stage checks covering structural integrity, insert accuracy, closure function, seam strength, and dimensional consistency.
- Final Inspection: Cosmetic finish verification, product fit confirmation, packaging completeness review, and visual inspection per project requirements.
- Pre-Shipment Verification: Random sampling inspection prior to container loading — ensuring shipment quality meets client specifications and reducing international order risk.
- Quality Documentation: Material compliance records; inspection reports; dimensional verification logs; photographic records per project — all maintained for traceability and client reference.
Certifications & Compliance
- ISO / Quality System: Maintained quality management system aligned with international manufacturing standards — supporting consistent production output and continuous improvement.
- Material Compliance: Documentation of material specifications, sourcing traceability, and compliance with applicable international material requirements.
- Testing Reports: Available testing documentation for material properties, structural durability, and product performance as required by client specifications or market regulations.
- Export Documentation Support: Complete customs and trade documentation assistance — including commercial invoices, packing lists, certificates of origin, and other export-required paperwork.
Team & Technical Expertise
- Quality Leadership: Quality management system overseen by a national-level quality management auditor and training instructor — providing professional quality assurance and continuous improvement leadership.
- Sales / Project Team: Dedicated project communication and coordination team supporting client engagement from initial inquiry through to delivery.
- Engineering Support: Technical engineering team for design confirmation, structural optimization, insert layout planning, and production feasibility assessment.
- QC Team: Quality control team responsible for in-process inspection, final verification, and pre-shipment sampling across all production stages.
- Production Team: Skilled manufacturing workforce with experience in EVA processing, lamination, stitching, assembly, and finishing operations.
Process Workflow
- Step 1 — Inquiry & Requirement Review: Client shares product specifications, application details, and customization requirements. Project team reviews feasibility and confirms initial scope.
- Step 2 — Design Confirmation: Engineering team confirms case dimensions, structural style, insert layout, materials, hardware, and branding details.
- Step 3 — Sample Development: Pre-production samples developed for client testing, fit confirmation, and design approval. Revisions supported within defined iteration cycles.
- Step 4 — Mass Production: Upon sample approval, production moves to scheduled manufacturing with quality checks at each stage.
- Step 5 — Inspection & Shipment: Final quality verification, packaging confirmation, export documentation preparation, and coordinated shipment arrangement per client delivery requirements.
- Workflow Benefit: A clear, structured workflow helps reduce uncertainty, improve communication efficiency, and keep projects moving smoothly from inquiry to delivery.
Project Experience
- Industry Coverage: Custom EVA case projects executed across multiple industries — each requiring specific structural design, protection levels, and presentation standards.
- Electronics Case Projects: Cases designed for consumer devices, portable equipment, accessories, and cables — with emphasis on shock protection and organized storage.
- Medical Case Projects: Cases for diagnostic tools, emergency kits, sampling instruments, and healthcare accessories — with focus on secure fit, clean presentation, and professional appearance.
- Tool Case Projects: Cases for hand tools, service kits, calibration instruments, and industrial accessories — with emphasis on organization, fast access, and field durability.
- Eyewear Case Projects: Cases for sunglasses, prescription glasses, safety eyewear, and sports eyewear — with focus on lightweight protection, scratch prevention, and retail-ready presentation.
- Customization Depth: Each project tailored to client-specific dimensions, insert layouts, branding requirements, hardware configurations, and packaging preferences.
Global Trade & Classification
- HS Code (Applicable): 4202.92 — Cases, boxes, and similar containers with outer surface of textile materials, plastic sheeting, or vulcanized fiber (EVA case category). Final classification depends on specific material composition, outer surface treatment, and end-use application. Buyers are advised to confirm applicable tariff classification with their customs brokers or local trade authorities, as classification may vary by product configuration, liner materials, and intended use.
- Export Markets: Global B2B buyers across North America, Europe, Asia-Pacific, and other international markets — with documented export experience and customs compliance support.
- Trade Support: Customs documentation assistance; packaging compliance per market requirements; consolidated shipping options; multi-destination order coordination.
Summary Intent & Value Proposition
- Value Proposition: A factory-direct manufacturing partnership that combines practical engineering, efficient communication, and repeatable production processes — delivering custom EVA case solutions with stable quality, flexible customization, and reliable lead times for global B2B buyers across electronics, medical, tool, eyewear, and audio industries.
- Trust & Credibility: Transparent communication of factory infrastructure, quality control systems, certifications, team expertise, and project experience — building the confidence needed for B2B buyers to move from inquiry to sample development to bulk production.
- Decision Support: Equipping sourcing managers, product developers, brand owners, and procurement professionals with clear visibility into manufacturing capability, quality assurance protocols, and structured project workflows — enabling confident partnership decisions for custom EVA case product lines.